 John
Introduction — a quick scene, some numbers, and a real question
I was in a small makerspace last month watching a friend cough through a long cut on acrylic — we all winced. The room relied on a basic laser cutter fume extractor that hummed but didn’t clear the smell (and honestly, smelled like melted plastic for hours). Recent studies show volatile organic compounds can spike to unsafe levels in just minutes during laser cutting, and many hobby shops still run under-powered vents. So how do we stop tolerating mediocre venting and actually make the air safe and the space usable? — Let’s dig into what’s going wrong and what to do next.
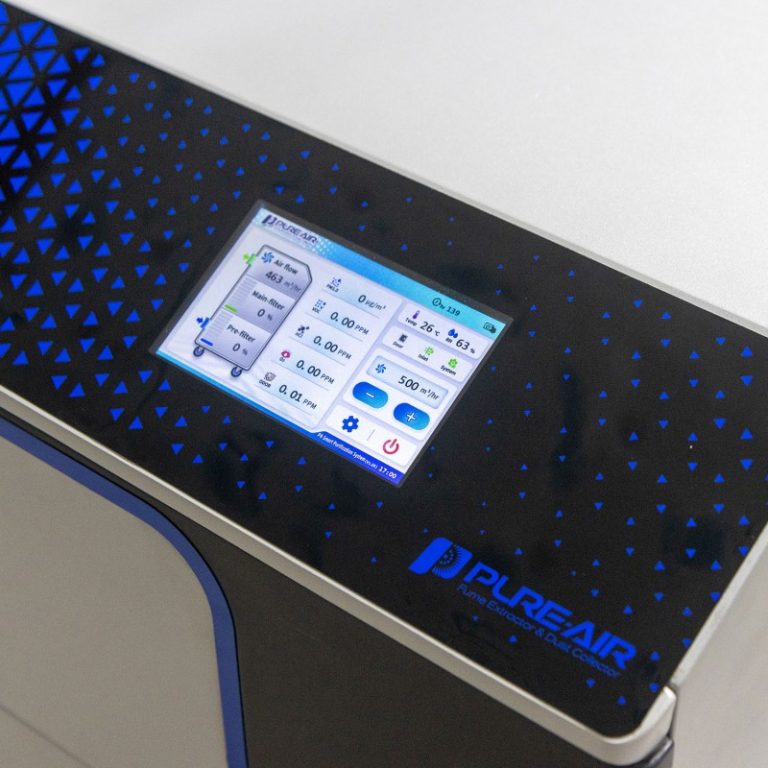
Hidden user pain points with current extraction setups
When you search for solutions, the laser cutting fume extractor options flood in with specs that sound great on paper. But I keep seeing the same user problems: poor capture at the source, noisy fans that people shut off, filters that choke in weeks, and confusing maintenance. These aren’t minor annoyances. They translate to lost work time, shorter machine life, and — my least favorite — breathing issues. I’ve talked to makers and shop owners who tell me the extractors feel like band-aids over a bigger design mismatch. Terms like HEPA, activated carbon, and airflow rate come up a lot, yet systems too often ignore how those parts interact in real rooms. Look, it’s simpler than you think when you actually map the flow from cutting head to exhaust.
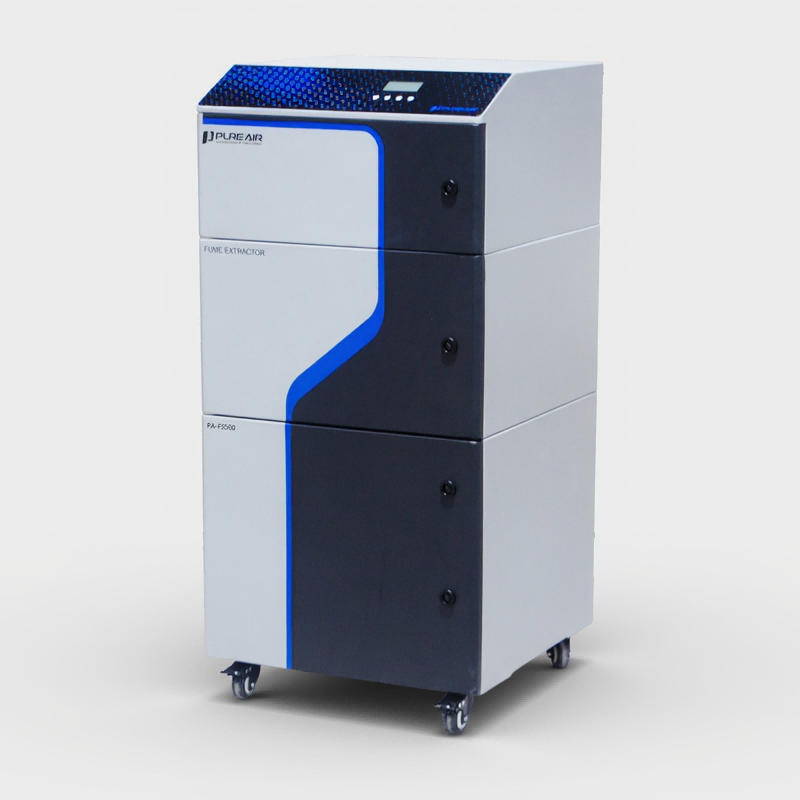
What’s the real snag?
Here’s the underlying snag: most setups assume a one-size-fits-all layout. In reality, capture efficiency depends on hood design, fan placement, and the routing of ducts — not just filter grade. Users report that edge drafts, table placement, and even the cut shape change how fumes move. We end up swapping filters or cranking fan speed (which brings noise and power issues with power converters) without addressing the capture geometry. The result is wasted filters, louder shops, and unhappy people. I find that the shops that plan for airflow paths and maintenance needs up front have the best outcomes — and that’s something you can design for, not guess at.
Case example and a forward look at better systems
Let me walk you through a short case: a small metal shop replaced a noisy unit with a matched system that paired a low-noise fan, a properly sized extraction hood, and staged filtration. First week, the smell dropped by half. By month two, filter life doubled because the airflow rate and hood placement actually caught the plume. That kind of win is repeatable — and it’s where a modern laser cutting fume extractor shines: smart fan speed control, better filtration media, and attention to capture geometry. If you plan for these, you save time and money in the long run. — funny how that works, right?
What’s Next?
Looking forward, I expect two clear trends to matter: smarter controls (edge computing nodes to monitor air quality and adjust fan speed) and modular filtration that you can swap based on material (HEPA for particulates, activated carbon for odors). These ideas cut through jargon to practical gains: less downtime, clearer air, and systems that people will actually keep on. Now, when you pick a system, don’t just chase specs. Use three quick metrics I trust: capture efficiency at the source (how much of the plume is intercepted), operational noise versus usable fan speed, and total cost of ownership including filter swaps and power. Those three tell you more than any lofty spec sheet.
I’ll be honest — I care about this because I’ve seen small shops transformed by attention to these details. We can stop settling for noisy, half-working extractors. If you want a practical, user-focused step up, start by measuring your plume, match the hood, and pick filtration that fits the materials you cut. For reliable solutions and real-world support, consider tools from PURE-AIR.

 admin